
Forced-induction systems turn ordinary intake plumbing into a pressure-management component. Turbocharger intercooler connections, supercharger bypass circuits, and throttle-body links may encounter positive boost, vacuum conditions, elevated intake temperatures, and oil mist from the compressor side.
In these locations, an extrusion hose must retain its shape and sealing performance while repeatedly moving between different pressure states. DEKUMA develops automotive tube extrusion technology around controlled material flow, dimensional measurement, and multilayer processing, providing a manufacturing context for the tighter requirements found in modern air-management systems.
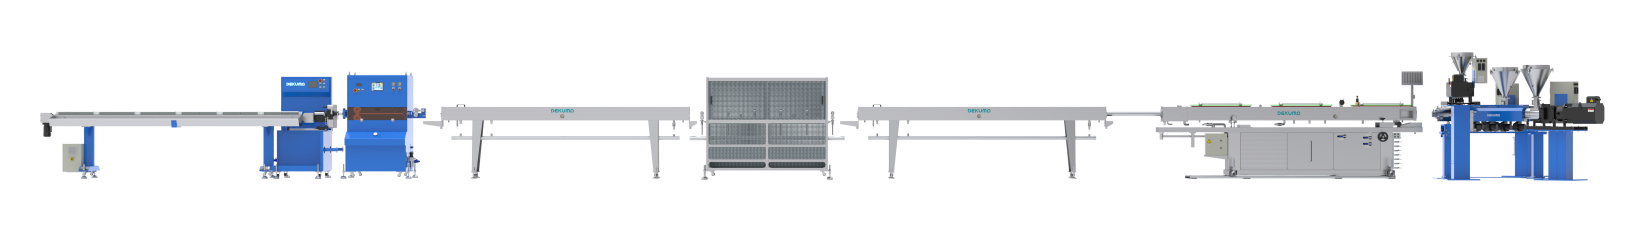
Pressure Cycles Change Hose Requirements
Boost pressure does not remain constant throughout vehicle operation. Rapid throttle changes can move the intake circuit from vacuum or low pressure toward positive boost, followed by pressure reduction during gear changes or throttle closure. Each transition places a different mechanical load on the hose wall, joints, clamps, and connection points. Repeated cycling can gradually expose weaknesses that may not appear during a static pressure test.
Turbocharger layouts introduce another variable: compressed air leaves the compressor at elevated temperature before passing through the intercooler. The downstream hose may experience cooler air, while the upstream section remains exposed to greater thermal loads. Expansion and contraction across these zones can affect dimensional stability, particularly where a flexible section connects rigid components.
Supercharger systems have their own duty pattern. Depending on the architecture, bypass valves can repeatedly shift the system between boosted and bypass conditions, creating frequent pressure transitions. Nylon extrusion can produce precisely dimensioned polymer tubing for selected automotive applications, although the suitability of nylon depends on the required flexibility, temperature range, pressure level, and compatibility with the surrounding system.
Oil Mist and Temperature Cycling
Boost air is not necessarily a dry, chemically neutral environment. Small quantities of oil mist can enter intake plumbing from compressor lubrication systems, crankcase ventilation routes, or other engine-bay sources. Long-term exposure may influence swelling, flexibility, surface condition, or adhesion in some polymer constructions, making fluid compatibility an important part of material selection.
Temperature cycling adds a second layer of complexity. A hose can move from relatively cool conditions after startup to significantly higher temperatures near a turbocharger, then cool again after the vehicle stops. Repeated thermal expansion can affect clamps and interfaces as well as the hose material itself. Local heat sources, radiant exposure, and airflow around the engine compartment should all be considered during specification.
Wall construction also affects behaviour under pressure. A thicker wall can provide greater resistance to deformation, while a multilayer structure may combine flexibility, mechanical strength, and chemical resistance. The appropriate design depends on hose diameter, bend radius, pressure differential, temperature, and connection method rather than wall thickness alone.
Extrusion Control and Dimensional Accuracy
Consistent wall geometry becomes particularly important around clamp and connector interfaces. Uneven thickness can create local stiffness differences, while dimensional variation may affect how securely a hose seats against a fitting. DEKUMA incorporates servo-controlled material feeding, specialized screw designs, and a multilayer composite die head within its automotive extrusion technology. Its downstream equipment can include ultrasonic wall-thickness inspection and laser diameter measurement, while servo-driven traction and cutting systems help maintain dimensional consistency during production.
Pressure stability inside the extrusion process also influences the finished tube. Fluctuations in melt pressure or material flow can translate into changes in wall thickness and surface geometry. A controlled servo drive can regulate layer extrusion more precisely, while the die design determines how individual materials are distributed around the tube circumference.
Maintenance has a practical effect on production consistency as well. A die head that can be disassembled and adjusted efficiently allows process teams to address deposits, dimensional drift, or configuration changes without unnecessarily extending downtime. DEKUMA’s stated design includes a die head intended for rapid adjustment by a single operator, alongside a touchscreen control interface and modular temperature regulation.
Matching Qualification to Forced-Induction Duty
Laboratory qualification should reproduce the pressure and temperature sequence that the hose will actually experience. Static burst pressure alone provides limited information about long-term behaviour because forced-induction plumbing is exposed to repeated loading rather than one isolated pressure event. Pressure cycling, thermal ageing, vacuum exposure, and dimensional checks can reveal different failure mechanisms.
Oil-mist exposure deserves its own test condition where the application warrants it. A material may tolerate dry-air cycling yet respond differently after prolonged contact with an oil-containing environment. Testing can examine changes in mass, dimensions, hardness, tensile properties, flexibility, and interface adhesion after controlled exposure.
Connection design is equally significant. Turbocharger and throttle-body hoses often depend on clamps, beads, quick connectors, or molded interfaces to maintain sealing during pressure changes. The finished hose must work as part of that assembly, with suitable bend behaviour and dimensional repeatability. Extrusion hose production can provide the controlled geometry required for such interfaces, but final qualification still depends on the complete vehicle installation and its operating cycle.
Conclusion
Forced-induction air circuits impose a combination of pressure reversal, heat exposure, oil-mist contact, vibration, and repeated thermal movement that makes hose design more demanding than simple air conveyance. Turbocharger and supercharger layouts also differ in their pressure patterns, so qualification should reflect the actual location and duty cycle rather than rely on one generic test profile.
Nylon extrusion offers one possible route for producing dimensionally controlled automotive tubing, while material formulation and construction must be matched to the application. DEKUMA‘s combination of controlled layer extrusion, dimensional inspection, servo-driven downstream equipment, and monitored temperature control provides a manufacturing framework for automotive hose development, with final suitability determined through application-specific testing.